Scaling packaging production can subject color and high quality issues that tiny runs hide. This guide discusses just how to systematize shade administration, substrates, authorizations, and QC before disparity ends up being an expensive brand name trouble.
A product packaging procedure that looks perfectly regulated at 1,000 boxes can become remarkably unstable at 100,000. Various manufacturing dates, providers, substrates, layers, printing pressures, drivers, moisture degrees, ink batches, and ending up processes begin pulling the end product in slightly various instructions.
And those distinctions gather.
I treat product packaging color consistency as a process-control trouble, not merely a design issue. A stunning authorized sample confirms that sample looked right. It does not verify that the 20th manufacturing run, a second supplier, or a various substrate will look the same 6 months later.
That is where several growing brand names get caught.
The tough fact? “Approved sample” is not a color management system.
At tiny quantities, individuals compensate for weak systems.
A designer checks the sample. A factory operator readjusts the press. A person compares the finished box versus an approved reference. If something looks somewhat off, the group speaks about it and fixes it.
That approach starts breaking down when production increases across numerous suppliers, centers, products, or nations.
The variables increase.
Product packaging color can be influenced by the substratum, ink formula, printing procedure, ink movie density, drying problems, covering, manufacturing rate, lighting, and also the condition of the physical color reference itself. X-Rite determines substrates, publishing processes, and ink kinds as significant variables influencing product packaging shade precision and consistency. X-Rite
So what happens when the same brand name color is published on layered paperboard in one center and a various board stock in one more?
You can have 2 practically qualified factories producing two noticeably various variations of the same brand name color.
That is not always a printer failing.
It may be a specification failure.
The first guideline of product packaging color monitoring is easy: develop what “right” actually indicates.
Without a taken care of target, every provider eventually creates its own analysis.
Pantone shade matching for packaging can offer a useful usual language, yet the recommendation requires to be appropriate for the actual product packaging application. Pantone’s own materials distinguish between graphic and packaging-specific shade systems, while its color-control solutions additionally emphasize quantifiable criteria and specified tolerances. Pantone +1
I would certainly define a master color spec having, where appropriate:
This matters due to the fact that “Pantone 123 C” on its own does not tell a production team every little thing it requires to know.
The substratum still matters.
The ink still matters.
The printing procedure still matters.
And the finished appearance issues more than a number sitting inside a layout file.
Below is an uneasy detail that obtains forgotten.
Your reference itself can transform.
Pantone notes that physical guides can come to be imprecise via handling, fading, improper storage space, and light exposure, and advises replacing guides roughly every 12– 18 months. Pantone Support +1
That produces a nasty manufacturing scenario.
A manufacturing facility contrasts today’s product packaging versus an old physical reference. The printer states the color matches. The brand group contrasts the outcome with a newer referral and states it does not.
Who is incorrect?
Perhaps neither.
The recommendation system has drifted.
For high-volume product packaging programs, I would as a result preserve regulated master references as opposed to enabling every provider to keep its own unofficial “gold sample.”
The referral needs to have an identifier, revision day, storage space demands, and clear instructions regarding when it have to be replaced.
Shade consistency starts before ink reaches the press.
If your product packaging uses numerous paperboards, coverings, laminations, metal films, or recycled materials, the same ink formulation can produce various aesthetic outcomes.
That is basic physics.
An extremely absorptive board can behave in different ways from a covered board. A warm substratum can shift perceived color. A matte covering can minimize aesthetic saturation compared to a gloss finish. Metallic or pearlescent surface areas introduce one more layer of intricacy.
This ends up being especially noticeable in costs stiff product packaging.
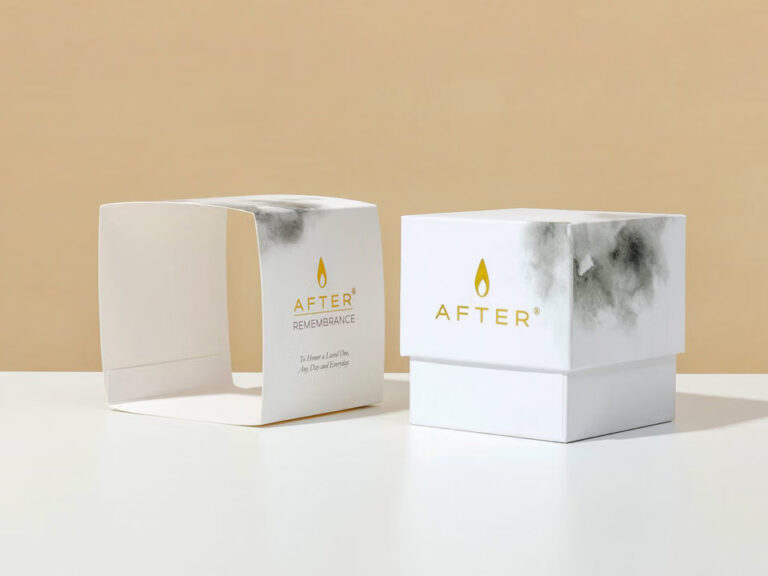
As an example, a gold foil magnetic clothing present box with pearlescent cover has a basically different aesthetic system from a traditional uncoated folding carton. The metal impact, reflective surface, foil, adhesive, and pearlescent product all affect just how the last shade is viewed.
So I would never ever define shade separately from substrate.
Define the combination.
Shade target + substratum + coating + process = manufacturing specification.
Aesthetic evaluation belongs.
It ought to not be the entire quality-control system.
Human vision adjustments with lighting, surroundings, fatigue, and specific assumption. Two experienced assessors can differ regarding whether a color is acceptable.
That is why batch-to-batch shade uniformity ends up being a lot easier to handle when aesthetic approval is sustained by objective measurement.
A spectrophotometer can evaluate shade as opposed to depending exclusively on a person claiming, “It looks a little darker.”
Delta E worths are typically made use of to reveal the mathematical distinction between 2 shades. The exact resistance that needs to be approved relies on the color, product, publishing procedure, brand requirements, and measurement approach.
The vital factor is not to consume over one global Delta E number.
The essential point is to specify your appropriate range before production.
That distinction matters.
A brand that states “match the example” has actually produced uncertainty. A brand name that defines a target, measurement problem, resistance, substrate, and authorization process has produced a repeatable system.
I choose multiple control entrances instead of one large examination at the end.
A practical product packaging quality-control process looks like this:
| Manufacturing Stage | What to Regulate | Typical Evidence |
|---|---|---|
| Artwork | Color specification, dieline, graphics | Accepted art work data |
| Prepress | Profiles, splittings up, trapping, place colors | Digital evidence |
| Tasting | Shade, substrate, ending up | Authorized physical example |
| Press setup | Ink, enrollment, thickness, shade target | Press sheet + dimensions |
| Manufacturing | Color drift, print defects, ending up | In-process QC records |
| Final inspection | Look, dimensions, building and construction | Inspection record |
| Shipment | Product packaging condition and quantity | Last QC approval |
The blunder is waiting until final evaluation to find that the shade has actually been wrong for 3 production days.
Already, you are not regulating top quality.
You are working out with waste.
Pantone works.
Yet Pantone alone will certainly not save a poorly managed manufacturing process.
The more powerful method is to connect the shade reference to actual manufacturing conditions.
Pantone defines certified printing programs that take a look at whatever from style and prepress with ink solution and pressroom processes, with standardized treatments meant to improve repeatability across production. Pantone
That viewpoint is important.
Shade consistency throughout production runs is not created by selecting a color code. It is developed by controlling the variables surrounding that shade code.
This comes to be a lot more crucial when multiple printing modern technologies are entailed.
Flexography, balanced out lithography, gravure, electronic printing, and specialty completing can replicate the exact same desired brand shade in different ways.
The requirements needs to make up that.
There works proof from business that have already encountered this problem.
In a 2023 study, Perfetti Van Melle defined a global packaging environment including labels, aluminum foil, paper, paperboard, and shrink sleeves across global printers. The firm implemented an electronic color-management approach using X-Rite Pantone devices to systematize color control across its network. X-Rite
The reported outcomes are exposing: X-Rite states PVM’s quality rating enhanced from 30– 35 in 2019 to over 60 in 2023, while the company expanded the use of dimension tools across its procedures. X-Rite
That is the lesson I respect.
The business did not solve a “pink problem” or a “blue trouble.”
It attended to the system responsible for producing color.
An additional instance originates from Asda, which handles greater than 12,000 SKUs and multiple packaging vendors. X-Rite records that Asda utilized ColorCert to approach purpose, quantifiable evaluation of print high quality instead of counting entirely on subjective assessment; its case study reports enhancements in high quality scores of up to 200%. X-Rite
Those numbers need to be treated as vendor-reported case-study outcomes rather than global industry benchmarks. But the operational concept is sound: as soon as top quality expectations end up being quantifiable, suppliers can be assessed against the exact same policies.
Color is only half the formula.
A box can have outstanding color uniformity and still look low-cost since the ending up top quality is irregular.
See:
For instance, premium precious jewelry product packaging may combine several of these variables in one item. A rigid double-door increased precious jewelry present box with display screen insert has far more top quality checkpoints than color alone.
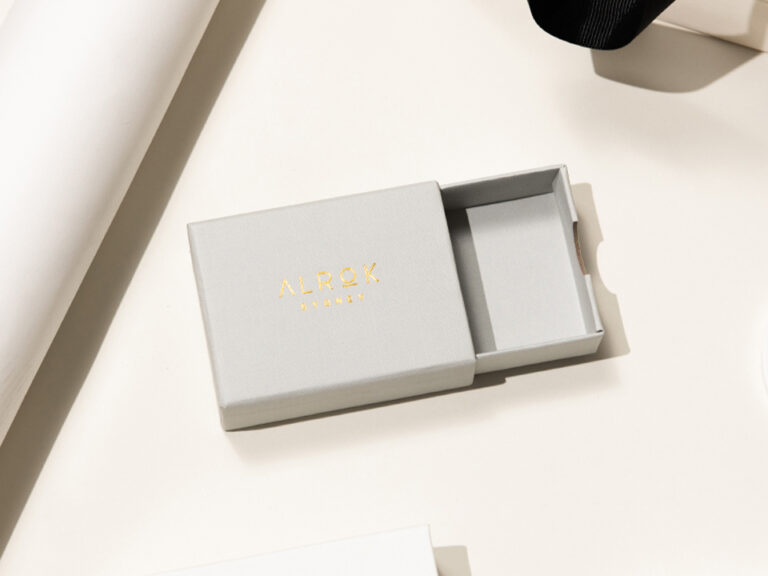
The same concept relates to a inflexible jewelry drawer box with gold foil and crystal handle.
When customers interact literally with costs packaging, issues become tactile.
They can feel them.
Once you have several suppliers, “great supplier” comes to be too vague to be valuable.
Procedure performance.
A vendor scorecard can include:
| KPI | What It Steps | Why It Matters |
|---|---|---|
| Shade pass price | Percent of production within tolerance | Measures consistency |
| First-pass authorization | Jobs accepted without correction | Discloses procedure security |
| Problem rate | Packaging issues per set | Measures physical quality |
| Remodel price | Manufacturing calling for correction | Indicates hidden costs |
| On-time shipment | Arrange reliability | Shields launches |
| Sample-to-production suit | Final result vs. approved example | Examinations scalability |
| Corrective-action closure | Speed of repairing repeating issues | Protects against rep |
This is where product packaging quality control comes to be management as opposed to inspection.
If Provider A produces lovely samples yet repetitively misses manufacturing resistances, that matters.
If Provider B produces a little less remarkable examples yet continually strikes the agreed spec, that matters also.
The numbers reveal the distinction.
Scaling internationally introduces one more problem: every location can progressively establish its very own analysis of the brand name.
One printer utilizes a slightly various ink formulation.
An additional alters the layer.
A third utilizes a various board.
A 4th assesses color under various lighting.
6 months later, you have 4 variations of the same brand name.
This is why digital color requirements and central specifications come to be important. Pantone’s very own products describe digital requirements as a means to develop mathematical shade referrals that can be interacted in between developers, printers, ink providers, and various other manufacturing companions. smart.pantone.com
The objective is not to eliminate regional production expertise.
It is to eliminate regional definitions of “close enough.”
This is just one of the extra controversial factors I would put in front of a packaging team:
A design that looks superb but is incredibly tough to reproduce constantly may be a bad manufacturing layout.
Not a bad creative layout.
A bad production style.
If a packaging concept requires five unique inks, 2 metallic results, a challenging substratum, several layers, very limited aluminum foil enrollment, and numerous finishing operations, every additional variable rises the number of means production can drift.
In some cases the smarter service is simplifying the process.
A metal drawer brow tweezer gift box with velvet insert highlights the contrary side of the equation: the packaging experience can still rely upon material, metal look, framework, and a premium insert while those elements are dealt with as purposeful manufacturing specifications rather than attractive second thoughts.
The goal is not minimal intricacy.
It is regulated complexity.
A scalable authorization process should respond to 5 concerns before automation begins:
If any one of those questions creates a various answer depending upon which supplier you call, the process is not standard.
I would certainly additionally maintain one master version of the spec.
Not five PDFs in five inboxes.
Not a photograph on WhatsApp.
Not “the sample we authorized last time.”
One controlled requirements.
That file should take a trip with the project from art work with manufacturing.
If you are relocating from small-batch packaging to significant production volume, I would certainly execute the system in this order:
Step 1: Lock the visual target.. Define the master color, substratum, layer, surface, and reference sample.
Action 2: Establish quantifiable tolerances.. Decide just how color and physical issues will certainly be measured prior to production starts.
Step 3: Standardize vendors.. Give every accepted factory the same technological requirements.
Step 4: Approve manufacturing samples.. Do not assume art work authorization amounts to making approval.
Step 5: Measure the first production run.. Capture unbiased data, not just photos.
Action 6: Display batch-to-batch variant.. Try to find patterns instead of waiting for evident failures.
Action 7: Document rehabilitative actions.. Every repeating flaw should generate a procedure change, not one more emergency situation meeting.
Tip 8: Audit regularly.. A procedure that operated at 10,000 units may require modification at 100,000.
For exceptional packaging programs, this framework ought to cover structure and finishing as well as shade.
A stiff competition match box with satin lining and ribbon, as an example, introduces material, bow, rigid-board building and construction, printing, and setting up into the high quality equation. Those aspects need to be specified and checked along with shade.
Product packaging color uniformity is not accomplished by asking a manufacturing facility to “make every set the exact same.”
That guideline is too vague.
Uniformity comes from criteria, measurements, controlled materials, defined resistances, repeatable processes, provider liability, and regimented approval gates.
The greatest product packaging operations do not depend on someone having an incredibly good eye.
They construct systems that make the proper outcome repeatable.
Which is the real difference in between product packaging that scales and product packaging that just endures its very first few orders.
Packaging color consistency is the controlled recreation of a brand name or product color throughout various product packaging sets, manufacturing dates, vendors, substratums, publishing processes, and locations while maintaining the finished appearance within an agreed visual and measurable resistance. It needs standardized color targets, products, dimension methods, lighting problems, and quality-control procedures.
Preserving product packaging shade consistency at range implies systematizing the color target, substrate, ink system, printing process, ending up specifications, dimension technique, and acceptable tolerance prior to manufacturing starts, then applying those same controls throughout every supplier and manufacturing area. Routine measurement and documented approvals avoid small distinctions from coming to be noticeable brand inconsistencies.
The most effective way to regulate batch-to-batch color uniformity is to compare every manufacturing batch versus one regulated master requirement using defined measurement problems and approval tolerances rather than counting entirely on aesthetic evaluation. This creates an unbiased pass/fail structure and makes shade drift less complicated to spot before huge quantities are finished.
Pantone gives standardized shade referrals and color-management tools, yet Pantone alone does not assure packaging color consistency due to the fact that final appearance depends on substratums, inks, printing processes, coatings, lighting, and production problems. Consistency requires applying the appropriate color criterion within a regulated production and quality-assurance process.
The same Pantone color can look different on different product packaging since substrate make-up, ink behavior, finish, publishing modern technology, ink film thickness, surface area texture, drying out conditions, and lighting can alter the resulting look. Pantone specifically notes that paper composition, inks, manufacturing speed, ink metering, and ecological aspects can add to visible variant. Pantone Assistance
Product packaging shade referrals should be replaced according to their material, storage space problems, usage, and the maker’s referrals, because physical references can fade or alter via handling and light exposure. Pantone currently advises changing its physical overviews around every 12– 18 months to help preserve trustworthy color interaction. Pantone +1
A packaging quality-control list should include color precision, substrate, print registration, surface area flaws, layer, foil or embossing positioning, architectural measurements, assembly, inserts, adhesives, hardware, and final look. The checklist ought to likewise determine the examination approach, acceptable resistances, sampling demands, accountable examiner, approval authority, and corrective-action treatment.
When product packaging moves from small manufacturing goes to large-scale production, high quality can not stay dependent on visual judgment and casual interaction.
The service is a regulated requirements that connects design intent with actual production.
Whether you are creating premium gift product packaging, fashion jewelry boxes, scent collections, clothing packaging, or personalized stiff boxes, the very same principle applies: define the target, regulate the variables, determine the result, and record the process.
If you are creating a brand-new product packaging program or preparing to scale an existing one, review the item formats over and use them as a starting factor for specifying your required shade, products, finishes, framework, and high quality requirements.