Sharp corners can conceal weak hinges. Learn how to specify residual greyboard thickness, challenge vague machine tolerances, and investigate cracking before approving a rigid box production run.
Sharp corners lie.
If a supplier offers a beautifully wrapped sample but cannot identify the board caliper, residual hinge thickness, cutting datum, or material batch behind it, I treat that sample as an attractive object with an unproven production specification.
What happens when the next pallet of greyboard arrives?
~에 대하여 rigid box V-grooving, the useful question is how much sound material remains beneath the groove—and whether production can hold that amount consistently. A deeper cut can make folding easier while leaving less material to survive handling. The neatest sample can sit dangerously close to that trade-off.
Greyboard V-grooving removes material along a fold line. Residual board thickness after V-grooving is the uncut material between the groove tip and the opposite board face, connecting the adjacent panels.
For a simple, unwrapped board section:
Cut depth = actual board thickness − residual board thickness
A measured 2.00 mm board with an approved 0.25 mm residual requires a 1.75 mm cut: 87.5% of its thickness. That is an arithmetic example, not a universal setting.
I would reject “cut 90% deep” as a complete specification. It says nothing about which fibres remain intact, whether a backing layer is included, or how the finished corner performs.
Specify the board grade, measured caliper, batch, grain orientation, and any layers bonded to it before grooving. Grammage in g/m² describes mass per area; it cannot replace a thickness measurement.
Also define the measurement boundary. A separately applied wrap is not part of the residual greyboard. If the board is laminated before cutting, identify the layers included in the residual measurement and which must remain continuous.
These decisions belong in the rigid box structural design and engineering specification, alongside groove position, corner geometry, and assembly requirements.
A machine brochure can quote an impressive number without telling you which dimension it controls.
For example, Standard Mechanical Works lists its XY-1200S V-grooving machine with a cardboard thickness range of 0.8–4.0 mm and “precision” of ±0.05–0.1 mm. The table does not define that figure as a guaranteed residual-thickness tolerance on finished sheets. standardmechanicalworks.in
My first question would be: precision of groove position, penetration depth, or remaining thickness?
Consider a hypothetical process with board caliper of 2.00 ±0.08 mm and penetration depth of 1.75 ±0.03 mm, measured from the upper face.
| Illustrative condition | Actual board thickness | Actual cut depth | Residual board thickness |
|---|---|---|---|
| Thinner board, deeper cut | 1.92 mm | 1.78 mm | 0.14 mm |
| Nominal dimensions | 2.00 mm | 1.75 mm | 0.25 mm |
| Thicker board, shallower cut | 2.08 mm | 1.72 mm | 0.36 mm |
These are worst-case combinations of hypothetical limits, excluding measurement uncertainty. They are not recommended production tolerances or predictions of how often either extreme occurs.
The resulting residual range is 0.14–0.36 mm, or ±44% around the intended 0.25 mm hinge. A modest-looking error on the full board becomes a large error in what survives the cut.
But the machine’s reference surface matters. Equipment that controls cutter clearance from a stable underside datum can respond differently to caliper variation. Ask how the machine establishes that datum, supports the sheet, and verifies the remaining material.
Specify and measure the finished groove. A display setting alone cannot establish the tolerance.
“The corner cracked” is a complaint, not a diagnosis. Cut open a rejected box and identify whether the fracture sits in the greyboard, wrapping paper, coating, laminate, or bond between layers.
In a 2012 TAPPI Journal study, Choi, Lavrykov, and Ramarao investigated delamination during paperboard scoring and folding. Their model was checked against microscopy and image-based strain measurements; excessive or uncontrolled layer separation could weaken the fold. College of Environmental Science and Forestry
A 2015 study by Tanninen and colleagues, published in BioResources and hosted by NC State University, examined folding control in paperboard tray forming. The researchers used 460 µm PET-coated board and tested creasing rules including 0.40 mm 그리고 0.71 mm widths; the narrowest rule required careful force adjustment because excessive force could cut through the coating. bioresources.cnr.ncsu.edu
Both studies concern creasing and folding rather than production V-grooving of rigid greyboard. They support investigating layer damage and tool–material interaction; they do 아니다 validate a particular residual thickness for your box. My practical inference is to judge the integrity of the remaining layers as well as their dimensions.
| V-grooving defects and symptoms | What I would investigate first |
|---|---|
| Cut-through or a split visible before wrapping | Minimum residual thickness, blade damage, sheet support, and local thin spots |
| Heavy folding resistance or a rounded corner | Excess residual material, groove geometry, trapped debris, and forming alignment |
| White fracture line confined to the wrap | Paper grain, coating or laminate damage, corner strain, and wrapping conditions |
| Layer separation near the groove | Board bonding, cutter condition, local cutting damage, and material conditioning |
| Cracking that appears after opening repeatedly | Hinge construction, adhesive bond, material fatigue, and the agreed opening cycle requirement |
These are investigation routes, not automatic verdicts. Forcing a corner closed can conceal the original problem and introduce another one.
Repeated opening deserves a separate hinge specification for magnetic closure rigid boxes 그리고 hinged-lid packaging. Identify which joints are folded during assembly and which must flex throughout use.
I would approve a process through a controlled trial, then retain enough evidence to reproduce it.
Use rigid box samples and pre-production prototypes to compare the lower, nominal, and upper proposed residual limits. Include representative material variation. One hand-selected success cannot establish the width of a usable process window.
The release record should state the approved residual range, measurement method, groove geometry, inspection frequency, and response to out-of-limit results. Verify again after blade replacement, setup changes, and material changes.
And keep rejected trial pieces. They show where the process starts to fail.
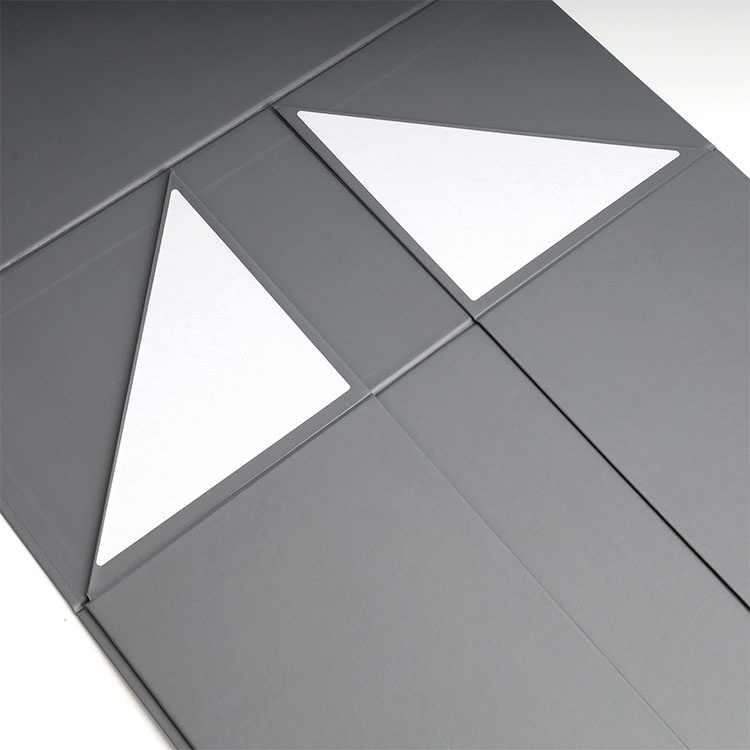
V-groove depth for rigid boxes is the distance from the cut face to the groove tip, calculated as actual board thickness minus the validated residual board thickness, so a 2.00 mm board with a proven 0.25 mm residual requires a nominal 1.75 mm cut.
The 0.25 mm figure is illustrative; validate the residual for the actual material and construction.
V-groove depth tolerances are the permitted deviations from a specified cut depth or remaining board thickness, and an acceptable limit must come from trials demonstrating reliable folding, intact backing fibres, stable assembled geometry, and satisfactory wrapped-box performance across the material variation expected in production.
State which dimension the tolerance controls and how it will be measured.
Rigid box corner cracking is a fracture of the greyboard, outer wrapping paper, coating, or laminate at a folded corner, potentially caused by local strain, material condition, groove geometry, cutting damage, or assembly conditions that must be distinguished before an operator changes the groove depth.
Inspect the failed layer before deciding whether to deepen or reduce the cut.
Preventing cracking when V-grooving rigid boxes means validating a residual-thickness range for the actual board and wrap, maintaining sharp and correctly aligned cutters, controlling material conditioning, removing groove debris, and confirming that production samples retain intact corners after assembly and the agreed handling tests.
Repeat the relevant checks when the material, tooling, or construction changes.
Contact XD Packaging to discuss your rigid box prototype with your box dimensions, product weight, intended board, wrap and finish, order quantity, and opening requirements.
Ask for a proposed residual-thickness range, groove cross-sections, and wrapped samples made near both proposed limits before approving production. Put the agreed measurement method and acceptance criteria into the specification.
Approve a corner you can measure—and a process that can reproduce it.